Abstract
This technical report provides a comprehensive evaluation of manganese phosphate coatings applied to 8620 and 9310 steel substrates, integrating data from Calico's internal coating documentation and the ASTM B117 salt spray test performed externally. The purpose of this report is to assess coating performance in terms of thickness, uniformity, corrosion behavior, and expected functional performance with and without oil post-treatment.
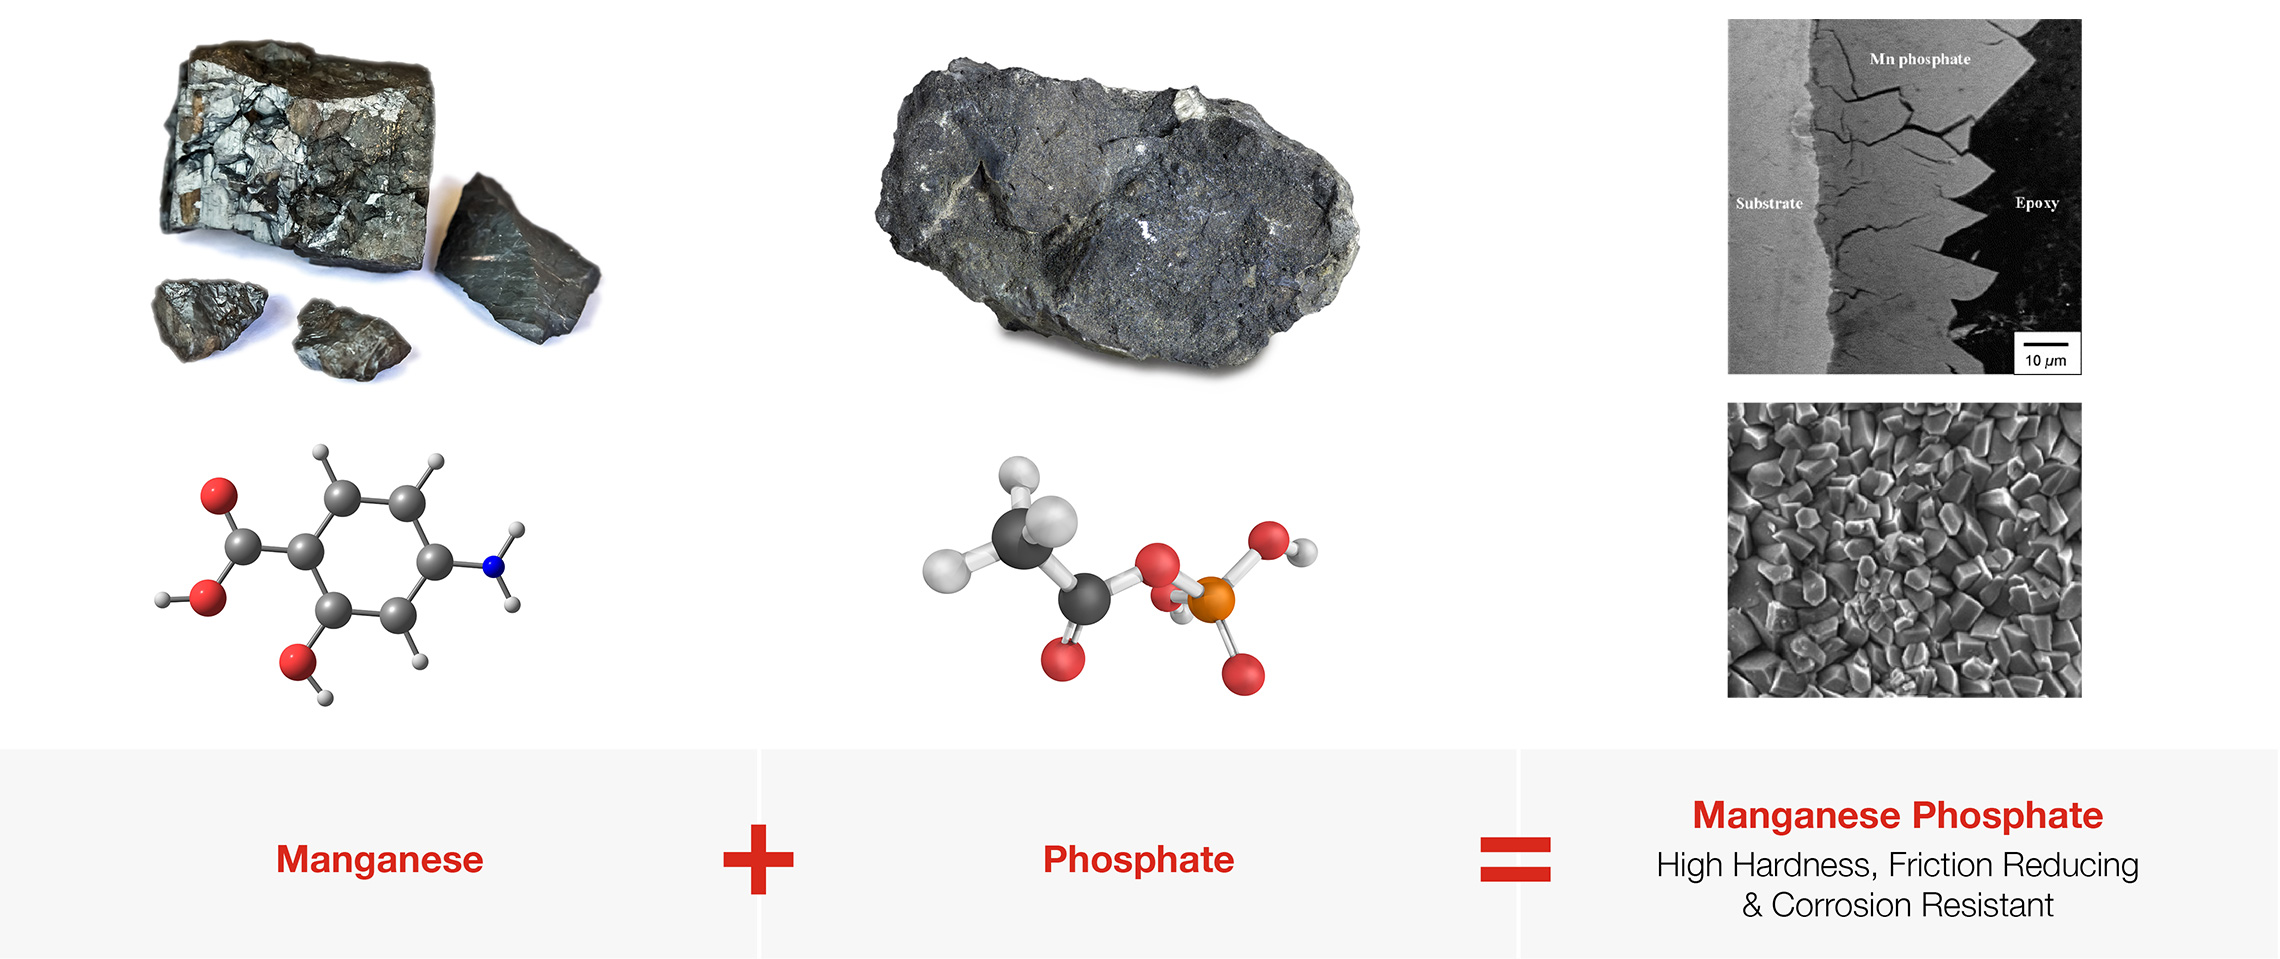
Manganese phosphate (Mn-Phos) is widely utilized in the automotive, firearms, aerospace, and tooling industries due to its ability to enhance wear resistance, reduce friction, and retain lubricating oils. Manganese phosphate is not intended as a standalone corrosion barrier, particularly in salt spray environments. This report explains why a supplementary protective layer — post-oiling and/or spray coatings — is advantageous.
1. Materials and Test Parameters
1.1. Substrates Tested
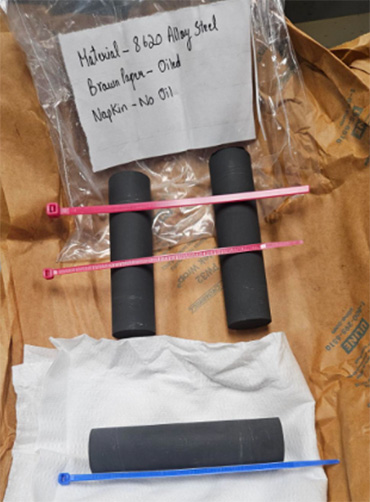
Steel Grades: 8620 and 9310
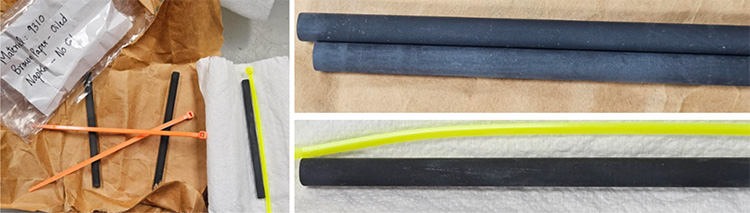
Sample Form: Cylindrical bar stock
Coating: Manganese phosphate
Post-Treatment Conditions: Oiled samples (after coating) and Non-oiled samples (baseline comparison)
1.2. Test Method
All samples were subjected to ASTM B117 Salt Spray (Fog) Testing for corrosion evaluation at two exposure durations: 24 hours and 48 hours
1.3. Chamber Operating Conditions (Reported)
All measured chamber parameters were within ASTM B117 compliance:
| Parameters | Observed Range | ASTM Requirements |
|---|---|---|
| Temperature | 94–95°F | 95°F ± 3°F |
| Air Pressure | 15 PSI | 12–18 PSI |
| Collection Rate | 1.79–1.91 ml/hr | 1–2 ml/hr |
| pH | 6.5 | 6.5–7.2 |
| Specific Gravity | 1.035–1.036 | 1.0255–1.040 |
The chamber conditions were stable and suitable for reproducible comparative testing.
2. Coating Thickness Evaluation
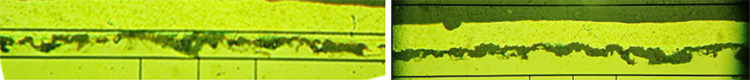
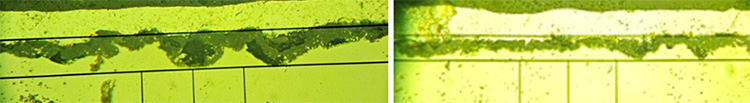
Cross-sectional coating thickness measurements were taken on non-oiled samples for both steel grades.
Measured Thickness Ranges
9310 Steel: 0.00026” – 0.00085”
8620 Steel: 0.00028” – 0.00080”
Interpretation
Typical manganese phosphate coatings exhibit thickness values in the range of: 0.0002” to 0.0010”
All values fall comfortably within this accepted range. Thickness variations are expected due to: Microstructural differences between 8620 and 9310, Surface roughness variability, Bath agitation and reaction kinetics, and Local steel chemistry influencing nucleation
No anomalies or failure indicators were observed in thickness results.
3. Corrosion Performance
3.1. Oiled Samples
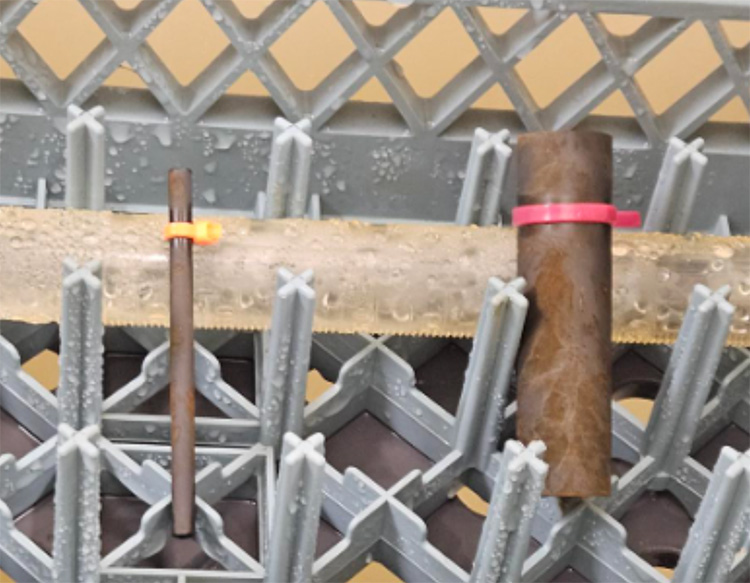
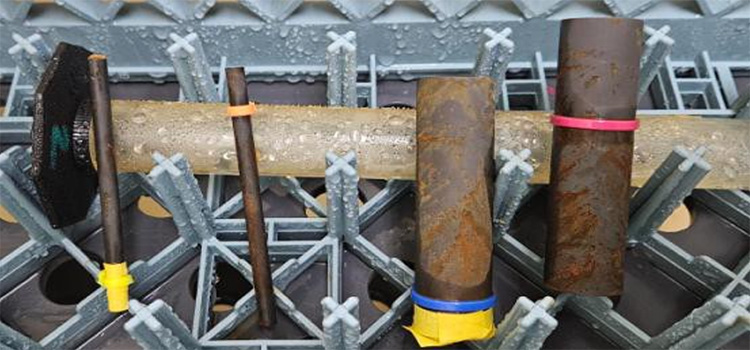
Oiled samples demonstrated: Delayed corrosion onset, More uniform surface preservation, and Improved protection throughout the test duration
This behavior is expected, as the manganese phosphate structure is highly porous and designed to retain oil. The oil becomes the true corrosion barrier, while Mn-Phos acts as the carrier.
3.2. Non-Oiled Samples
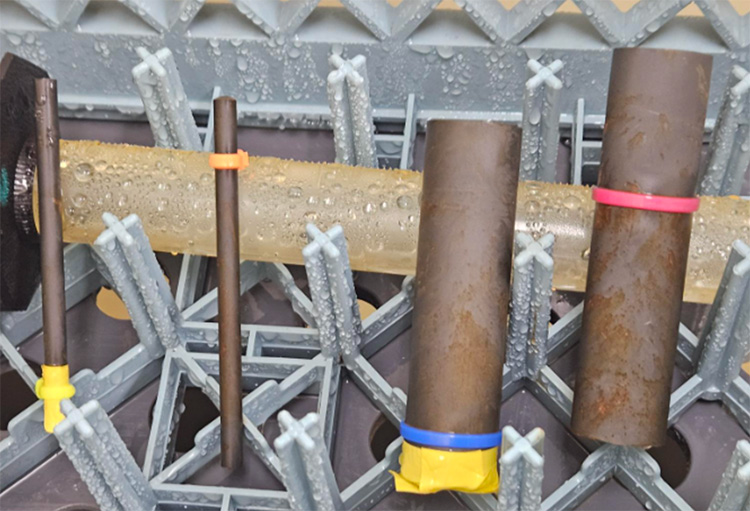
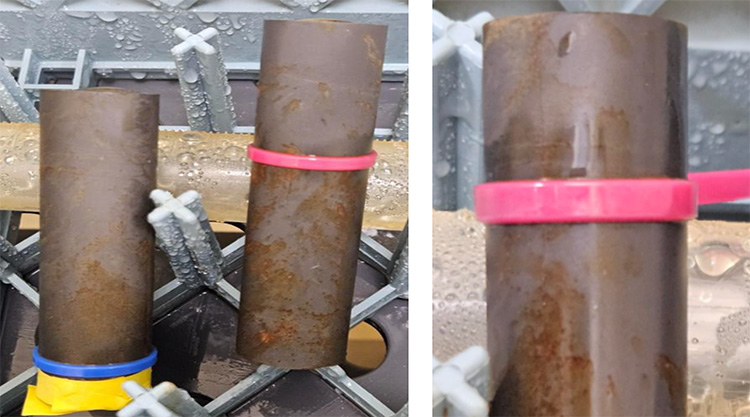
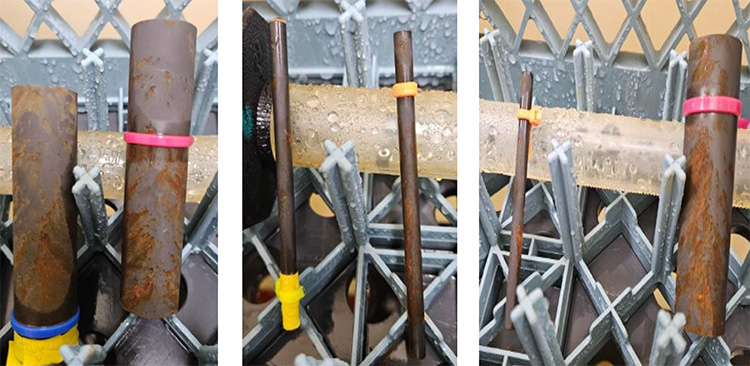
Non-oiled samples exhibited: Rust initiation visible at 24 hours and Significant corrosion by 48 hours on both alloys
The corrosion performance reflects correct coating behavior—not coating failure.
4. Technical Assessment
4.1. Functional Role of Manganese Phosphate
Mn-Phos is engineered for: Wear resistance, Friction reduction (excellent boundary lubrication), Break-in protection, and Oil retention
4.2. Coating Microstructure & Corrosion
Mn-Phos creates a porous crystalline matrix, enabling it to: Absorb oils, Hold lubricant films, and Improve scuff resistance
These pores also provide pathways for rapid corrosion when no oil is present. Thus, corrosion on bare Mn-Phos is expected and unavoidable.
4.3. Validation of Coating Quality
The following indicators confirm a healthy coating process: Thickness values are within specifications, Oiled samples show extended protection, Non-oiled samples behave exactly as industry standards predict, and No anomalies or uneven crystalline growth were reported.
5. Conclusion
The manganese phosphate coatings applied to 8620 and 9310 steel parts exhibit normal and expected behavior consistent with industry standards.
Conclusions Supported by Data
Coating thickness values fall within proper specification ranges. Oiled samples demonstrate effective corrosion delay, proving the coating's proper porosity and oil retention capability. Non-oiled samples corrode within 24–48 hours, which aligns with the known behavior of Mn-Phos systems. No evidence of coating failure, improper chemical preparation, or deviation in coating quality was observed.
Overall Assessment
The manganese phosphate coating line appears to be: Stable, Consistent, and Producing coatings that perform as designed
6. Result
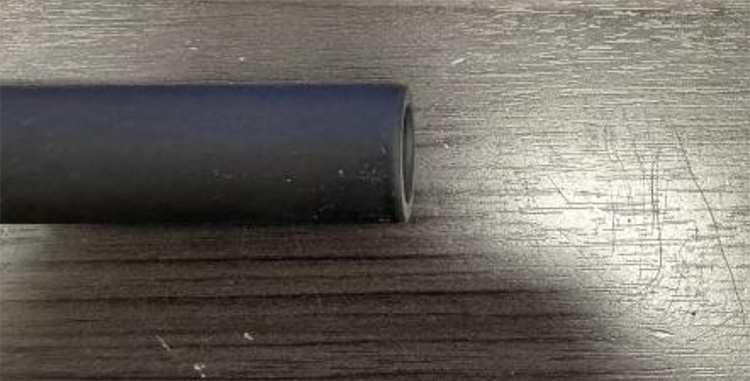
In addition to the B117 salt-spray results, long-term field evidence corroborates the coating's effectiveness: a production component coated using the same Mn-phosphate process has remained rust-free after more than one year in real operating conditions, validating both the coating chemistry and the oil-retention mechanism beyond laboratory testing.