Home/Services/Superfinishing & Microfinishing

Superfinishing & Microfinishing

Isotropic surface finishing eliminates directional lay and reduces roughness to a mirror-like finish using two methods — vibratory polishing and centrifugal force microfinishing.

2
Process Methods
2
Finish Types
Isotropic
Surface Result
Technology Overview
Isotropic Surface Finishing

Calico's superfinishing and microfinishing processes transform ground or machined surfaces into optimized tribological interfaces. Unlike traditional machining that leaves directional tool marks (lay), these processes produce isotropic surfaces — with no preferred directionality — that dramatically reduce friction, wear, and noise in mating surface applications.

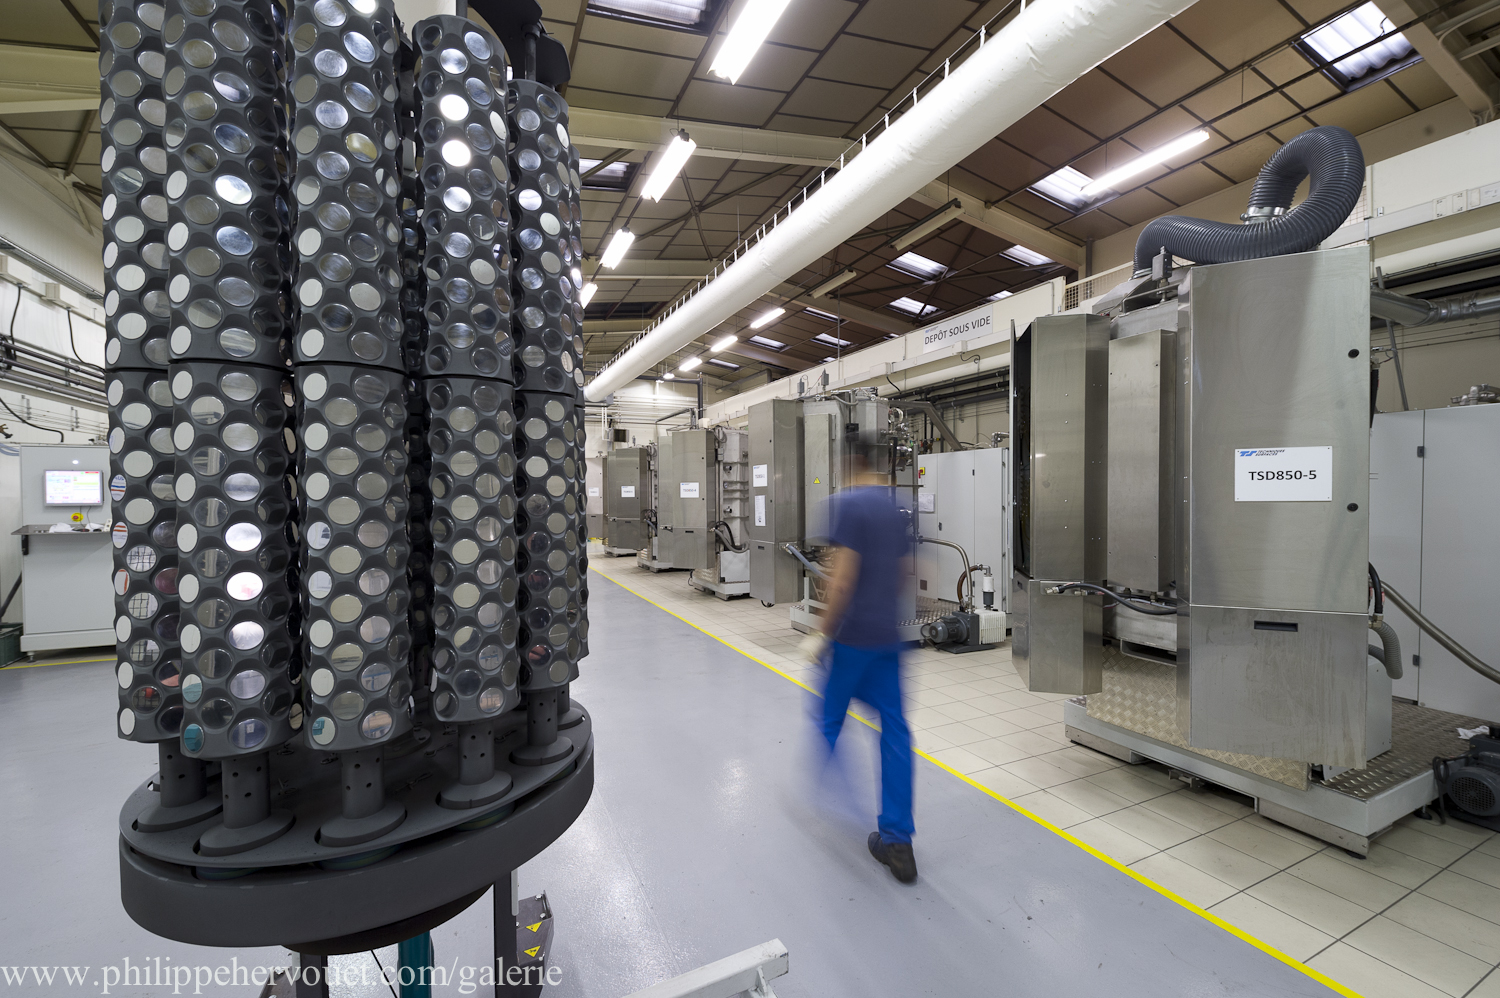
Two complementary methods are employed. Vibratory polishing uses ceramic media and proprietary compounds in a vibratory bowl to refine surfaces through controlled mass finishing. Centrifugal force microfinishing applies centrifugal energy to dramatically accelerate the process for precision components with tight geometry requirements.

Superfinishing uses a two-step approach: the refinement phase forms and removes an oxide layer while mechanically polishing the peaks, followed by a burnishing phase that produces the final bright, uniform surface. The result is a part with significantly lower Ra values in the valleys, and superior load-carrying capacity — with no material removal from chemical attack or heat distortion from grinding.

2
Process Methods
2
Finish Types Available
Process Overview
Precision at Every Step
Step 01
Surface Preparation
Parts are cleaned and inspected prior to processing. Surface condition and dimensional requirements are reviewed to select the appropriate method, media, and compounds for the desired finish type.
Step 02
Refinement
The refinement phase combines formation and controlled removal of an oxide layer with mechanical polishing of surface peaks. This removes grinding lay, reduces Ra, and prepares the surface for burnishing.
Step 03
Burnishing
The burnishing phase produces the final bright, isotropic surface finish — uniform in all directions with no directional tool marks. Finish level is controlled by media selection and process time.
Step 04
Final QC
Surface roughness measurement (Ra) and visual inspection confirm the target finish specification is achieved.
Why Superfinish
Advantages of Isotropic Finishing
Isotropic Finish
No directional lay means uniform load distribution across mating surfaces, reducing localized stress concentrations that initiate wear and micro-pitting in gear and bearing applications.
Mirror-Like Surface
Dramatically reduced Ra values improve oil film retention in the surface valleys while polished peaks reduce friction — resulting in lower operating temperatures and extended component life.
Improved Efficiency
Creates a uniform, non-directional surface that reduces roughness, friction, and surface imperfections — helping components run more efficiently, extend service life, and improve overall performance.
Short Cycle Times
Both vibratory and centrifugal methods process batches of parts simultaneously — delivering high throughput and short lead times while maintaining consistent finish results across the full batch.
Finish Options
Available Surface Finishes
* Finish type and Ra target are determined in consultation with our applications engineers based on substrate material, part geometry, and tribological requirements.

Ready to Engineer Your Advantage?

Talk to our applications engineers about how isotropic superfinishing can reduce friction, extend component life, and improve system efficiency.
Tech Line: 704.483.2202
Request a Consultation